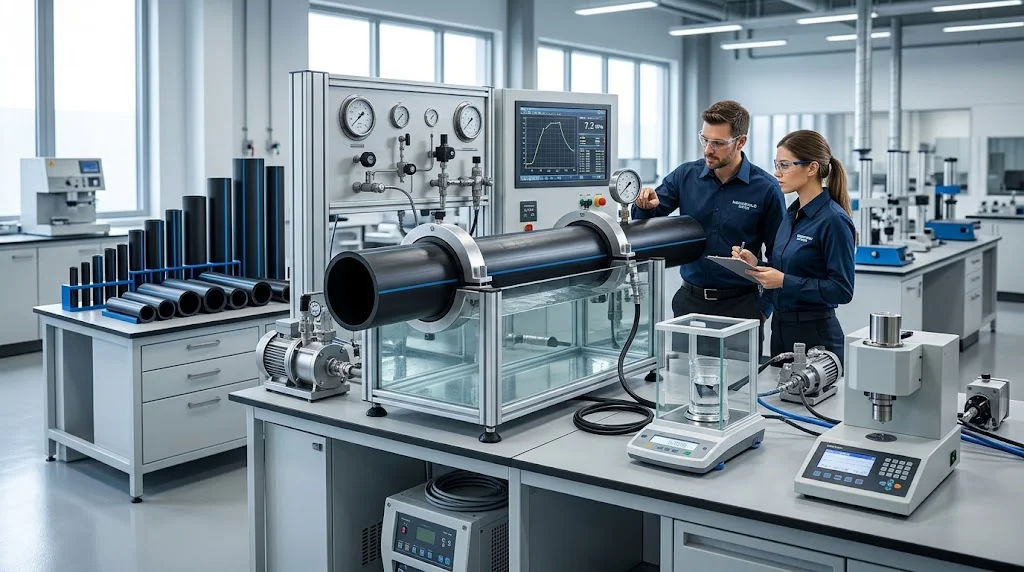
Picture two coils of black 110 mm pipe sitting side by side on a site in Lahore. Same colour, same printed stripe, similar price. One will carry water for decades. The other may weep at a joint in year three, or crack under a pressure surge nobody planned for. From the outside, you cannot tell which is which.
That is the job of HDPE pipe testing. A short list of laboratory checks, including hydrostatic strength, melt flow index and density, turns a black plastic tube into a documented, comparable product. After installation, a field pressure test shows whether the finished pipeline holds together. This guide explains what each test measures, how to read the numbers on a pipe test report, and which questions are worth asking before you accept a delivery.
Two kinds of HDPE pipe testing
Most confusion starts here, so it is worth separating them.
Laboratory (factory) tests check the pipe and the resin it was made from. Samples are taken from production batches and measured against a product standard such as ISO 4427 for water pipe. These tests answer one question:
was this pipe made correctly?
Field tests are done on site after the pipeline is laid and jointed. They answer a different question:
was this pipeline installed correctly? The Plastics Pipe Institute (PPI) is clear that field testing is not meant to replace or supplement the product-standard tests, so one never substitutes for the other.
| Test |
Common method |
What it tells you |
Where it happens |
| Hydrostatic strength |
ISO 1167 |
The pipe resists internal pressure over time |
Factory lab |
| Melt flow rate (MFI) |
ISO 1133 |
The resin grade is on spec and was not damaged in processing |
Factory lab |
| Density |
ISO 1183 |
The material is what it claims to be (a screening check) |
Factory lab |
| Carbon black content and dispersion |
ISO 6964, ISO 18553 |
Sunlight protection is present and evenly mixed |
Factory lab |
| Oxidation induction time (OIT) |
ISO 11357-6 |
Enough antioxidant is left for long service life |
Factory lab |
| Field hydrostatic test |
ASTM F2164 or pressure rebound method |
The installed pipe, joints and fittings hold pressure |
On site |
Hydrostatic pressure testing In the laboratory: can this pipe carry pressure for decades?
Short lengths of pipe are sealed, filled with water and held at a fixed pressure in a water bath. Nobody can wait 50 years to find out whether a pipe lasts 50 years, so laboratories raise the temperature, which speeds up ageing. ISO 4427-2 sets the hoop stress each grade must survive at each temperature. For the 2007 edition, as summarised by a pipe supplier’s technical guide, the PE100 figures are:
| Test condition |
PE100 hoop stress |
PE80 hoop stress |
| 20 °C, 100 hours |
12.4 MPa |
10.0 MPa |
| 80 °C, 165 hours |
5.4 MPa |
4.5 MPa |
| 80 °C, 1,000 hours |
5.0 MPa |
4.0 MPa |
Each test uses three test pieces, and none may fail during the period.
Stress is not pressure. The pressure a laboratory applies depends on the pipe’s wall thickness. Using the standard relationship, pressure = 2 × stress ÷ (SDR − 1), a 110 mm SDR 11 PE100 pipe (a PN 16 pipe) tested at 12.4 MPa stress at 20 °C sits at about 2.48 MPa, or roughly 24.8 bar, for 100 hours. At 80 °C and 5.4 MPa stress the same pipe is held at about 10.8 bar. These are our own worked examples using the standard formula, so check the figures against the edition your specification cites.
Brittle versus ductile failure. A pipe that fails by cracking in a brittle way early in the test points to a material problem, and that is exactly why a good report states the failure mode if there is any failure at all.
In the field: was the pipeline installed correctly?
PPI Technical Note TN-46 covers field hydrostatic testing of HDPE pressure pipelines. A few points matter to anyone supervising a test:
- HDPE creeps under pressure. The pipe expands slightly, so pressure in a sealed section drifts down. PPI stresses that this self-limiting behaviour is normal for plastic and is not by itself a sign of a leak. That is why HDPE tests differ from tests on rigid metal pipe.
- Air and temperature spoil results. Fill slowly, vent the high points, and allow the line to settle to a stable temperature before testing. PPI suggests a rest of roughly 3 to 24 hours depending on the volume of water.
- Test pressure is a multiple of the rating. PPI describes test pressures typically between 1.25 times the operating pressure and 1.5 times the design pressure rating of the weakest component in the section. Pressure is measured at the lowest point.
- Two accepted methods. ASTM F2164 holds pressure for 4 hours, topping up water as needed, then drops the pressure slightly and watches for 1 hour, passing if pressure stays within 5%. The pressure rebound method is a shorter alternative that also accounts for the pipe’s elastic recovery.
- A pass is not a lifetime guarantee. PPI notes leaks can still appear later, so the hydrotest is one tool among several.
Requirements on Pakistani projects follow the contract specification, so confirm the test method and pressure with your engineer or the utility. For gas lines the procedure differs again; see our guide to
HDPE pipes for gas distribution in Pakistan.
Melt flow index (MFI): what the flow tells you about the resin
Melt flow rate (often still called melt flow index) measures how many grams of molten polymer pass through a standard die in 10 minutes, under a fixed weight and temperature. For pipe-grade PE100, the usual conditions under ISO 1133 are 190 °C and 5 kg.
Pipe resin is deliberately slow-flowing. Long, tangled polymer chains give toughness and resistance to slow crack growth, and they flow slowly. Typical PE100 compound datasheets from major resin makers list values around 0.17 to 0.25 g/10 min at 190 °C and 5 kg. A much higher number suggests shorter chains, which means a different material or a degraded one.
MFR does two jobs on a test report:
- It identifies the compound. The pipe’s result should sit close to the resin supplier’s declared value.
- It catches processing damage. Overheated or reprocessed material changes its flow behaviour. ISO 4427-2:2007, as summarised by a pipe supplier, limits the change between compound and finished pipe to within ±20%, which makes MFR a useful check for regrind or an over-hot extruder.
Watch the test conditions. The same material gives very different numbers at 2.16 kg and at 5 kg. A report that quotes an MFR without temperature and load is not comparable with anything.
Density: a quick screening check, not proof of grade
Density is measured under ISO 1183 by weighing a sample in air and then in a liquid of known density. Black PE100 compounds typically list about 960 kg/m³ (0.960 g/cm³) on resin datasheets, with the carbon black contributing to that figure.
Why it is useful: a density well outside the expected band can hint at a different resin, a blend with a lower-grade polyethylene, or added filler. Why it is not enough: two very different polyethylene grades can share a density. Density cannot tell PE80 from PE100, and neither can your eyes. Both look identical at the same SDR, and the difference lives in the pipe marking, the resin certificate and the strength tests. Treat density as a screening step, never as the whole story.
Other lab checks that appear on a good report
- Carbon black content and dispersion. Black PE100 compounds typically contain about 2.0 to 2.5% carbon black, with dispersion rated 3 or better. This is what protects pipe from sunlight, and poor mixing weakens it.
- Oxidation induction time (OIT). This measures how much antioxidant remains after processing. Many datasheets quote at least 20 minutes. A pipe can pass pressure tests today and still age badly if it is under-stabilised. Check the test temperature stated against your edition of the standard, since resin datasheets often use 210 °C while the 2007 edition of ISO 4427-2 uses 200 °C.
- Elongation at break and longitudinal reversion. These show ductility and whether extrusion stress is locked into the pipe. The 2007 edition lists at least 350% elongation at break and no more than 3% reversion.
- Outside diameter, wall thickness and out-of-roundness are checked against the standard’s tolerances and the SDR you ordered. See our SDR rating guide for how SDR links to pressure rating.
How to read an HDPE pipe test report
A test report is only useful if it relates to the pipe in front of you. Work through these steps:
- Find the laboratory and the standard. Note who issued the report, whether it is in-house or third-party, and which standard and edition it names (for example ISO 4427-2).
- Match the product. The diameter, SDR, material grade and batch or lot code on the report should match the marking printed on your pipe. A report with excellent numbers for a different batch is a document-control failure, not quality assurance.
- Check the test conditions. Look for temperature, stress or pressure, duration and, for MFR, the load. Numbers without conditions cannot be compared.
- Compare results with requirements. Good reports show the requirement next to the result and a clear pass or fail. If only results appear, ask for the limits.
- Look for the failure mode. For hydrostatic tests, ask whether any test piece failed and how.
- Check dates and signatures. The test date should fall within a sensible window of production, and the report should be signed and numbered.
- Cross-check the pipe marking. Pipe made to ISO 4427 should carry the standard, manufacturer, dimensions, SDR, material designation (PE100 or PE80), pressure rating and a production date or batch code, printed along the pipe at regular intervals.
Red flags: a generic datasheet instead of a batch report, a report for a different size, missing test conditions, results with no limits, and no way to trace the pipe to a batch.
Newtech’s own buying guides tell buyers to request batch test certificates and PSQCA documentation up front, because chasing paperwork after delivery delays handovers and payments. For a wider checklist of delivery checks see our
HDPE pipe price guide and the
PSQCA and ISO 9001 certification guide.
ISO 9001 & PSQCA Certification Guide
NewTech Pipes · Quality & Certification
Collecting batch reports before you accept a delivery? Read NewTech’s guide to ISO 9001 and PSQCA certification and what to check in the paperwork.
Read Guide
What testing cannot tell you
Honest limits are part of good quality control:
- Samples are not every metre. Laboratory tests represent a batch, which is why traceability from report to batch to pipe matters so much.
- Looks prove nothing. Appearance cannot confirm grade, so rely on marking, resin certificates and reports.
- Pipe tests do not cover joints. Most service failures in HDPE systems trace back to joints, so fusion quality and fittings matter as much as pipe quality. Trained crews and well-maintained butt-fusion equipment make a real difference.
- A passed hydrotest is a snapshot. It confirms the line is sound today, not that it can never leak.
Why this matters in Pakistan
Two local realities make testing documents more than paperwork.
First,
heat. ISO 4427 pressure ratings apply at a 20 °C reference temperature and fall as the pipe warms. During Pakistani summers, shallow or above-ground lines can run far hotter than that, so ask for the derating factors and check your working pressure against them rather than the headline PN.
Second,
procurement. Utilities, developers and consultants often expect PSQCA-marked pipe with traceable batch certificates before they accept material on site. A complete, readable test report is how you pass that gate on the first try instead of the third.
Conclusion
Every supplier will tell you their HDPE pipe is strong. Hydrostatic strength, melt flow and density are how that claim becomes a number you can check. Learn what each test measures, make sure the report matches your batch, and treat the field hydrotest as the final proof of your own installation.
If you remember one thing, make it this: ask which batch the report covers. Everything else follows from that.